Fire Resistant Cables
Fire resistant cables are designed to maintain electrical circuit integrity during a fire, ensuring that critical systems continue to operate when they are needed most. In emergency situations, cable performance is determined not only by flame resistance, but also by the ability to withstand extreme temperatures while maintaining power or signal transmission. At the same time, factors such as smoke emission, halogen content, mechanical durability, and compliance with international fire safety standards play a crucial role in cable selection.
We recommend considering a custom fire resistant cable whenever system availability during a fire is essential or when demanding fire safety regulations must be met. Habia develops fire resistant cables by optimizing conductordesign, fire-resistant insulation systems, material selection, shielding concepts, and cable geometry to achieve the required level of fire performance without compromising electrical or mechanical reliability. The result is a cablesolution engineered to maintain circuit integrity under fire conditions while delivering dependable long-term performance throughout its service life.
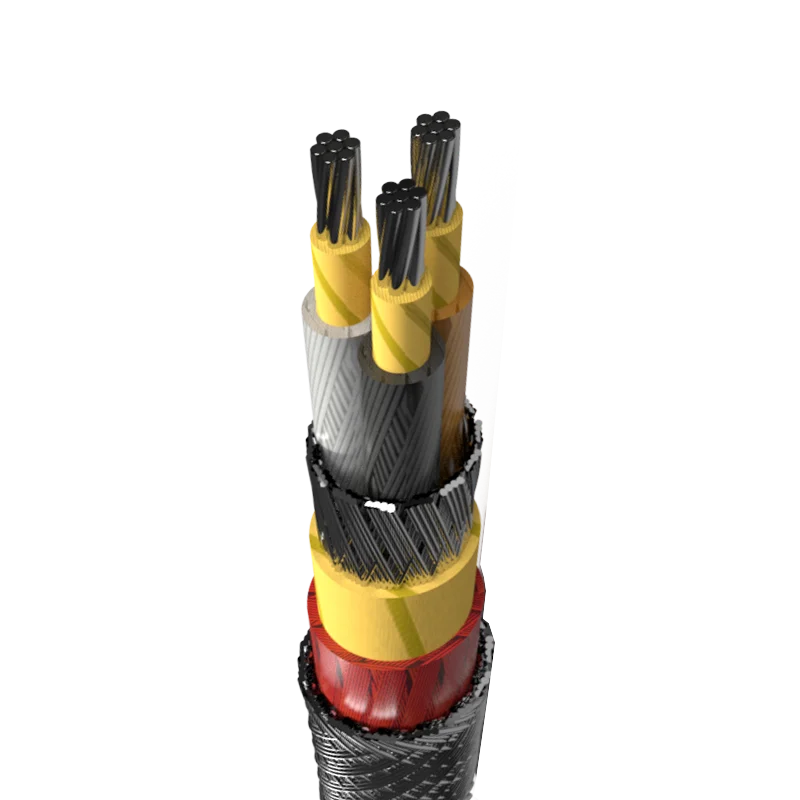
The Unique Strengths of Habia Cables and Habia as a Cable Manufacturer
The performance of a fire resistant cable depends on far more than its ability to resist flames. Maintaining circuit integrity under fire conditions requires the precise combination of conductor design, fire-resistant insulation systems, material selection, shielding concepts, and cable geometry. At the same time, factors such as smoke emission, halogen content, mechanical durability, environmental resistance, and compliance with international fire safety standards must all becarefully balanced to meet the requirements of the application.
With decades of experience in specialty cable engineering and manufacturing, Habia supports customers from the earliest stages of product development. Our engineering teams evaluate fire performance requirements, operatingconditions, installation constraints, environmental influences, and applicable industry standards to develop a technically and commercially optimized cable solution. This collaborative development process simplifies system integration, reduces development risk, and helps ensure long-term operational reliability. The result is a custom-engineered fire resistant cable that maintains critical power or signal transmission during fire conditions while delivering dependableperformance throughout its entire service life.
Insulation and Jacket Materials for Fire Resistant Cables
Selecting the right insulation and jacket material is essential to the fire performance and long-term reliability of a fire resistant cable. In addition to maintaining electrical performance under normal operating conditions, the materials must withstand extreme temperatures, limit flame propagation, reduce smoke emission, and, where required, maintain circuit integrity during a fire. Drawing on decades of expertise in specialty cable engineering, Habia selects the optimum material combination to meet the specific fire safety, electrical, mechanical, and environmental requirements of each application.
-
Silicone Rubber
Silicone rubber is one of the most widely used insulation materials for fire resistant cables due to its outstanding thermal stability and its ability to maintain electrical insulation at elevated temperatures. It is the preferred choice wherecircuit integrity during fire conditions is essential.
-
Mica Tape
Mica tape provides exceptional fire resistance by forming a highly effective thermal barrier around the conductor. It is widely used in fire resistant cable constructions to help maintain circuit integrity during direct flame exposure.
-
PTFE
PTFE (Polytetrafluoroethylene) combines exceptional dielectric performance with outstanding resistance to high temperatures and aggressive chemicals. It is recommended for fire resistant cable designs requiring long-term reliability in demanding thermal environments.
Applications for Fire Resistant Cables
Fire resistant cables are used wherever electrical circuits must continue to operate during a fire to support life safety, emergency response, or critical industrial processes. In these applications, maintaining circuit integrity under extreme temperatures is just as important as minimizing flame propagation and smoke generation. Habia develops fire resistant cables that combine reliable electrical performance with compliance with demanding international fire safety requirements.
Railway & Transportation
Rail vehicles, tunnels, and transport infrastructure require cable solutions that combine fire resistance with low smoke and halogen-free performance. Habia develops fire resistantcables that support passenger safety while ensuring reliable operation under demanding conditions.

Marine & Offshore
Ships and offshore installations require fire resistant cables capable of maintaining electrical functionality while minimizing smoke and corrosive gas emissions. Habia developscable solutions that meet the demanding safety requirements of marine environments.

Energy & Power Generation
Power plants and critical electrical infrastructure require cables that maintain circuit integrity during fire events to support essential monitoring, control, and emergency systems. Habia develops fire resistant cables engineered for reliable long-term performance in demanding energy applications.


Your Custom Cable, Right at Your Fingertips
Your Custom Lightweight Cable
Developing a fire resistant cable involves far more than selecting flame-resistant materials. Maintaining circuit integrity during a fire requires the precise combination of conductor design, fire-resistant insulation systems, thermal barriers, material selection, and cable geometry. Every application has unique requirements regarding fire performance, operating conditions, installation constraints, and regulatory compliance. Habia develops fire resistant cablesengineered to meet these requirements without compromising electrical performance or long-term reliability.
From the initial concept and material selection through prototype development, qualification, fire testing, and series production, Habia supports every stage of the development process. Our engineering teams optimize conductorconstruction, insulation systems, fire-resistant materials, and cable design to develop solutions that maintain reliable power or signal transmission under fire conditions while delivering excellent mechanical durability during normal operation. The result is a custom-engineered fire resistant cable that integrates seamlessly into the final product, supports compliance with demanding fire safety standards, and provides dependable long-term performancethroughout its entire service life.


